Updated October 13, 2026. Rebuilt from 5 problems to 10, with every fix checked against the printer makers’ own guides and the settings Nick uses in his videos.
Some links on this page are affiliate links. If you buy through one, Planet 3DP earns a small commission at no extra cost to you. It never changes what we recommend. How this works. As an Amazon Associate I earn from qualifying purchases.
Most failed prints come down to a short list of causes. A dirty plate, wet filament, too much speed or a cold room. This guide sorts the ten problems you’re most likely to hit by when they show up, so you can find yours fast and fix the cause, not the symptom.
Each fix comes from the printer makers’ own help pages, mostly Bambu Lab and Prusa Research, plus the slicer settings from Nick’s own print farm. Try the fixes in the order listed. The first one is usually the cheapest.
This guide covers filament (FDM) printers. Resin printers fail in different ways. If you’re still choosing, start with FDM vs resin printing.
Find your problem fast
Start with when the print went wrong. That one fact rules out half the causes.
| When it fails | What you see | Check first | Go to |
|---|---|---|---|
| First layer | Lines won’t stick, get dragged or peel up | A dirty plate or the wrong plate type | 1. First layer |
| First few layers | Corners lift and curl | Bed too cool, fan on too early | 2. Warping |
| Any time | Fine hairs between parts | Wet filament | 3. Stringing |
| Any time | Gaps between lines, weak walls | Dirty extruder gears | 4. Under extrusion |
| Any time | Little or nothing comes out | Heat creep or debris | 5. Clogs |
| Any time | Rough, pitted or stringy walls | Moisture in the spool | 6. Wet filament |
| Middle | The print steps sideways | Too much speed | 7. Layer shifts |
| Halfway or near the top | Tall prints wobble, shift or stop | Sway as the print gets taller | 8. Fails halfway |
| Under overhangs | Supports topple, spaghetti | Supports with a tiny footprint | 9. Supports |
| Finished print | Ripples and rough outer walls | Outer wall speed | 10. Rough walls |
1. The first layer won’t stick
What it looks like: lines that don’t fuse, get dragged around by the nozzle, or peel up partway through. Everything above the first layer depends on it, so fix this first.
Why it happens: oil on the plate from your fingers, the wrong plate type picked in the slicer, a bed that’s too cold, or a first layer printed too fast.
How to fix it, in this order
- Wash the plate. Bambu Lab says to clean the A1 textured plate with warm water and regular soap. Prusa calls 90% or stronger isopropyl alcohol the best degreaser for a quick wipe, and dish soap with warm (not hot) water when that stops working. Prusa only uses acetone on smooth PEI, about once a month.
- Pick the right plate in the slicer. A wrong plate type means a wrong bed temperature. Bambu Lab lists around 35°C for PLA on its Cool Plate and around 55 to 65°C on its Textured PEI Plate.
- Add heat. Prusa suggests raising the bed 5 to 10°C for materials that won’t stick.
- Slow the start. Prusa suggests about 75% speed for the first three layers.
- Use glue only where it helps. Prusa says PLA doesn’t need it. Glue can help with PETG, ABS, ASA, nylon, polycarbonate and flexible filament.
One thing not to do: Prusa warns against lowering Live Adjust Z to make up for poor adhesion. Set too low, it can damage the sheet.
Cold garage? Nick’s winter fix is a second filament preset with the initial layer bed temperature 5°C higher (65°C to 70°C on his textured plate), saved with “Winter” in the name. If your garage drops into the teens (°F), he says to build an enclosure.
2. Corners curl up (warping)
What it looks like: the corners lift off the plate and the part starts to rock. Sooner or later the nozzle catches an edge.
Why it happens: Bambu Lab points to the wrong bed temperature or plate type first. Layers that cool too fast pull on the layers below them. A cold room makes it worse, even with PLA and PETG.
How to fix it, in this order
- Check the plate and bed temperature (see problem 1).
- Cut the cooling at the start. Bambu Lab says most filaments should have no part cooling for the first 3 layers, and suggests turning the auxiliary fan down to about 40 to 50%.
- Warm up a cold room. Below 20°C, Bambu Lab suggests raising the bed about 10°C and keeping drafts off the printer.
- Change the infill on big parts. Bambu Lab suggests gyroid over straight line patterns and says to avoid going over 50% infill.
- Add a brim. A brim adds a wide ring of plastic around the base that holds the corners down. Brim ears add small pads only at the corners, so cleanup is quicker.
- Match the material to the printer. Bambu Lab recommends an enclosed printer for ABS, ASA, PC and nylon. PLA warps so little it’s fine on an open frame printer.
3. Stringing and oozing
What it looks like: fine hairs or webs between parts of the print, left behind as the nozzle travels.
Why it happens: Bambu Lab lists damp filament first. Then long travel moves with short retraction, a nozzle that’s too hot, and a large nozzle.
How to fix it, in this order
- Dry the filament (see problem 6). It’s the most common cause, so rule it out first.
- Lower the nozzle temperature 5 to 10°C and print again, as Prusa suggests.
- Check retraction. Bambu Lab generally recommends no more than 2 mm, because too much retraction can cause a clog. Prusa uses a 2 mm maximum on its MK3 family. Bowden printers like the Prusa MINI use more (3.2 mm by default).
- Turn on Avoid crossing walls in the slicer, which keeps travel moves inside the part.
- Foaming filament such as LW PLA needs its own settings. Bambu Lab suggests a flow ratio between 0.5 and 0.7 and a lower temperature.
Already printed? Prusa’s cleanup trick is a heat gun at about 200°C for one or two seconds. Any longer and the part can deform.
4. Gaps and weak walls (under extrusion)
What it looks like: Prusa describes it as material missing from your layers. You see gaps between lines, thin walls and parts that snap easily.
Why it happens: dirty or misaligned extruder gears, an idler screw that’s too loose or too tight, heat creep, a partial clog, wet filament, or filament that’s out of spec. Prusa gives plus or minus 0.05 mm as the industry standard for diameter.
How to fix it, in this order
- Clean the extruder gears and check the idler tension.
- Rule out a partial clog (see problem 5).
- Steel nozzle? Prusa says hardened or stainless nozzles usually need 5 to 10°C more heat.
- Purge properly when you switch filament. Prusa loads the new filament at the old filament’s temperature, so leftover plastic gets pushed out.
- Measure, don’t guess. Nick checks flow by printing a 20 mm calibration cube and measuring it with calipers. If the sizes are off, so is your extrusion.
5. Little or nothing comes out (clogs and heat creep)
Why it happens: Bambu Lab lists a hotend that isn’t hot enough, and tiny particles from filled filaments like wood that build up at the nozzle tip. The sneaky one is heat creep. Heat moves up into the cold side of the hotend and the filament softens before it should.
Bambu Lab says heat creep mostly hits PLA and TPU in enclosed printers, and PETG when the enclosure runs too hot.
How to fix it, in this order
- Let heat out. Bambu Lab says to keep the inside of an enclosure at least 10°C below the filament’s glass transition temperature. For PLA it suggests printing with the front door and top cover off, and its material table recommends removing the top glass when the bed is above 45°C.
- Push it through hot. For PLA, Bambu Lab’s method is to set the nozzle to 250°C and feed filament by hand.
- Clear debris with a cold pull, which Bambu Lab recommends after carbon fiber filaments in particular.
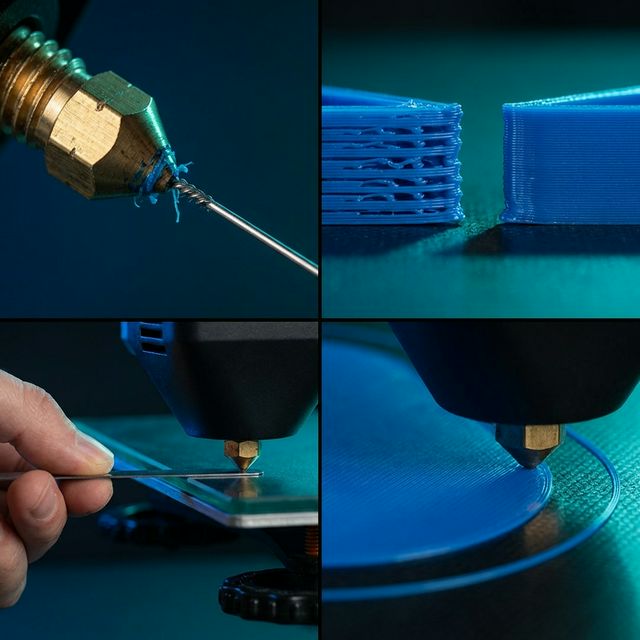
Nick's go to: an extruder unclogger rod. He heats the hotend to 270°C, makes sure there’s a clear path down through the extruder, and gently pushes the rod down. Often there’s a pop and the filament comes out of the nozzle.
Free failure prevention cheat sheetEvery slicer setting from this guide on one printable page. Keep it next to the printer.
Get the cheat sheet6. Wet filament: stringy, rough and weak
Filament pulls moisture out of the air. Bambu Lab lists what that does to a print: stringing, missing material, holes, rough surfaces and lower strength. A spool that printed fine last month can start doing all of that in a damp week.
Drying fixes it. Bambu Lab and Prusa don’t agree on exact numbers, so here are both. If your spool’s label says something different, follow the label.
| Filament | Bambu Lab (drying oven, 8 h) | Prusa (Prusament) |
|---|---|---|
| PLA | 50 to 60°C | 45°C for 6 h |
| PETG | 60 to 70°C | 55°C for 6 h |
| TPU | 65 to 75°C | 60°C for 4 to 6 h |
| ABS and ASA | 75 to 85°C | ASA: 80°C for 4 h |
| PC | 75 to 85°C | PC Blend: 85°C for 5 h |
| Nylon (PA) | 75 to 85°C, 8 to 12 h | PA11 Carbon Fiber: 90°C for 6 h |
Keep it dry after. Bambu Lab says most filaments need under 20% relative humidity to stay dry for long. At around 55% humidity, freshly dried filament can start picking up moisture again within about 2 to 12 hours. Prusa stores spools in a closed box or a vacuum bag with desiccant.
No dryer? Bambu Lab’s method for PLA on its enclosed printers is the heated bed at 65 to 75°C for 12 hours, covered with a box and flipped every 6 hours.
What Nick uses: a Sunlu S4. It holds four spools, goes up to 70°C and starts and stops on its own based on humidity, and you can feed printers straight out of it.
Buying direct from Sunlu? Use code MRNGB2VN5D at checkout for a discount.
7. The print steps sideways (layer shifts)
What it looks like: the layers stop lining up and the print jumps sideways in X or Y. Small shifts look like a staircase.
Why it happens: people blame belts first, but Nick finds it’s often speed. A fast toolhead carries a lot of momentum into tight corners. Prusa’s list adds loose belts, a loose pulley set screw, something blocking the bed or toolhead, and overhangs that curl up until the nozzle crashes into them.
How to fix it, in this order
- Slow the walls. Nick’s starting point is the outer wall speed and the small perimeter speed down by about 20 to 25%. Prusa also suggests slower speeds for large objects.
- Check for anything in the way of the bed or toolhead, including cables.
- Check the belts. With the printer cold and off, move each axis by hand. Prusa says a tight belt sounds like a low bass note when you pluck it.
- Check the pulleys. Each pulley’s set screws need to be tight, with one sitting on the flat part of the motor shaft.
- CoreXY printer? Move the toolhead along both diagonals too. Prusa says a rough diagonal points to that diagonal’s motor or pulley.
8. Tall prints wobble or fail halfway
A tall or skinny print starts fine because the base has plenty of grip. As it grows, every move, every speed change and even the fans add a little sway at the top. The sway adds up, layers stop lining up, and the top can shift or break off. It hits bed slingers like the A1 hardest, and anything with a small footprint.
How to fix it, in this order
- Slow down only the top. Bambu Studio’s Slow Down by Height setting changes speed and acceleration between a start height and an end height, so the base still prints fast.
- Use gyroid infill on tall parts, thin walls and anything that flexes. It has no weak direction, so it resists the wobble. It prints slower than triangles or grid.
- Add a brim (see problem 2) so the base stays planted.
| Nick’s dragon bust example | Start | End |
|---|---|---|
| Height | 38 mm | 250 mm (the top) |
| Speed | 250 mm/s | 125 mm/s |
| Acceleration | 6,000 mm/s² | 1,000 mm/s² |
| Print time | About 9.5 hours before | A little over 12 hours after |
If the printer stops itself: a mid print error isn’t always the print. Nick’s Snapmaker U1 threw a false power off error two days into a job. The fix in Snapmaker’s wiki is in Advanced Mode: raise the power loss detection threshold. He moved his from 0.022 s to 0.04 s and the print ran clean.
Watch: the slicer settings that stop most failures
Nick walks through layer shifts, Slow Down by Height, modifier meshes, brims and brim ears, support expansion and infill choice in Bambu Studio.
9. Supports fall over or the print turns to spaghetti
Spaghetti is what you get when something lets go and the printer keeps printing into the air. Often it’s a support. A support with a small footprint can wiggle, shift or fall over, and in a cold room supports are usually the first thing to fail.
How to fix it, in this order
- Give supports a brim. In Bambu Studio this is the initial layer expansion setting on the support tab. Nick uses 8 mm for most medium and tall prints and 10 mm or more for big parts like helmets and cosplay pieces.
- Fix the first layer and warping first (problems 1 and 2). Most spaghetti starts there.
- Reinforce one weak spot with a modifier mesh. Drop a cube over the area and change infill, walls or speed inside it only.
10. Ripples and rough outer walls
What it looks like: faint ripples after sharp corners (ringing), wavy or bumpy outer walls, or steppy curves.
Why it happens: speed and vibration. When the toolhead moves too fast on the outer wall it shakes a little and lays the line down unevenly.
How to fix it, in this order
- Slow the outer wall. In his smoother prints video, Nick cuts outer wall speed by 50 to 100 mm/s for parts that need to look their best.
- Print the outer wall first. Set Order of walls to outer then inner, so the visible line doesn’t get pushed by the walls next to it.
- Test Avoid crossing walls on and off if you see blobs on the walls.
- Use variable layer height for curved models. Thin layers go only where the model curves, so you get smooth curves without doubling the print time.
- Run the printer’s calibration. Bambu Lab’s calibration includes vibration compensation along with bed leveling.
Six more problems, fast
| Problem | What you see | Fix this first |
|---|---|---|
| Elephant’s foot | The first layer flares out wider than the rest | Turn on elephant foot compensation (Bambu Studio: Process, Quality). Bambu Lab says it comes from the soft first layer being pressed down by the weight above. |
| Messy, irregular layers | Rough layer lines that wander side to side | Bambu Lab says a loose nozzle is the usual cause. On the A1 and H2D, check the hotend clip. On X and P series printers, check the nozzle fixing screws. |
| Even lines down the sides | Ridges repeating up the walls | Simplify3D says a 5% change in filament diameter can change line width by up to 0.05 mm. Try better filament, and check that the hotend holds within 2 degrees. |
| Multicolor won’t load | The AMS fails to feed or unload | Bambu Lab’s first checks: the spool turns freely, no tangle, no sharp bend in the PTFE tube above the toolhead, no damaged connector. |
| Colors bleed | Streaks of the old color after a change | Bambu Lab says going from black to white needs several times more flushing than white to black. Don’t flush into infill when printing transparent filament. |
| Slow decline on fiber filament | Under extrusion that creeps in over weeks | Carbon fiber and glass fiber filaments need a hardened steel nozzle, and Nick counts glow in the dark filament as abrasive too. Bambu Lab says to avoid 0.2 mm nozzles with them and makes 0.6 mm the first choice. |
Most of these come back to maintenance. Planet 3DP has model by model guides for the A1, P2S, H2S, H2C and X2D.
Common questions
Why does my 3D print fail halfway through?
Usually it’s height. Tall prints sway more as they grow, so the top shifts or a support lets go. Slow the top of the print with Slow Down by Height, give supports a wider base, and on enclosed printers rule out heat creep with PLA.
Why is my 3D print stringy?
Bambu Lab lists damp filament as the first cause. Dry the spool, then lower the nozzle 5 to 10°C and keep retraction at or under 2 mm on direct drive printers.
Why won't my print stick to the bed?
Most of the time the plate is dirty or the slicer has the wrong plate type. Wash the plate with dish soap and warm water, pick the right plate, add 5 to 10°C of bed heat and slow the first layers.
How do I know if my filament is wet?
Bambu Lab lists stringing, missing material, holes, rough surfaces and weak parts. The easy test is to dry the spool and print the same part again.
Do I need glue on the build plate?
Not for PLA, according to Prusa. Bambu Lab says the A1’s textured plate prints PLA, PETG and TPU without glue. Glue can help with nylon, polycarbonate, ABS and ASA.
Is a layer shift always a hardware problem?
No. Speed is a common cause, so lower the outer wall and small perimeter speeds first. If it keeps happening, check the belts, the pulley set screws and anything in the toolhead’s path.
Watch Planet 3DP on YouTubeNew printers, slicer updates and hands on tests every week.
Subscribe- Bambu Lab Wiki: Filament guide material table (checked October 13, 2026)
- Bambu Lab Wiki: Stringing and oozing (checked October 13, 2026)
- Bambu Lab Wiki: Printed model warping (checked October 13, 2026)
- Bambu Lab Wiki: Heat creep (checked October 13, 2026)
- Bambu Lab Wiki: Drying filament (checked October 13, 2026)
- Bambu Lab Wiki: Nozzle clog (checked October 13, 2026)
- Bambu Lab Wiki: Elephant foot compensation (checked October 13, 2026)
- Bambu Lab Wiki: Severe layer artifacts (checked October 13, 2026)
- Bambu Lab Wiki: AMS loading and unloading failures (checked October 13, 2026)
- Bambu Lab Wiki: Reducing waste during filament changes (checked October 13, 2026)
- Bambu Lab Wiki: Printer calibration (checked October 13, 2026)
- Bambu Lab Wiki: A1 FAQ (checked October 13, 2026)
- Prusa Knowledge Base: First layer issues (checked October 13, 2026)
- Prusa Knowledge Base: Stringing and oozing (checked October 13, 2026)
- Prusa Knowledge Base: Under extrusion (checked October 13, 2026)
- Prusa Knowledge Base: Layer shifting (checked October 13, 2026)
- Prusa Knowledge Base: Drying filament (checked October 13, 2026)
- Simplify3D: Lines on the side of print (checked October 13, 2026)
- Planet 3DP video: Your 3D Prints Keep Failing (Jan 10, 2026) (checked October 13, 2026)
- Planet 3DP video: Fix Winter 3D Printing Problems (Dec 11, 2025) (checked October 13, 2026)
- Planet 3DP video: The 1 Slicer Setting That Fixed My Print (Nov 1, 2025) (checked October 13, 2026)
- Planet 3DP video: 5 Easy Bambu Studio Settings for Smoother Prints (Dec 6, 2025) (checked October 13, 2026)
- Planet 3DP video: New 3D Printer? Don't Start Without These Tools (Apr 23, 2026) (checked October 13, 2026)
- Planet 3DP video: Open Source 3D Printer Saves the Print (Jul 29, 2026) (checked October 13, 2026)
- Planet 3DP video: I Ran All 3 Of The Best Beginner 3D Printers (Aug 22, 2026) (checked October 13, 2026)
Host of Planet 3DP. I’ve been 3D printing for over four years, with tens of thousands of print hours on Bambu Lab, Anycubic, Creality, Elegoo and Snapmaker machines. Planet 3DP on YouTube.
Last checked October 13, 2026.